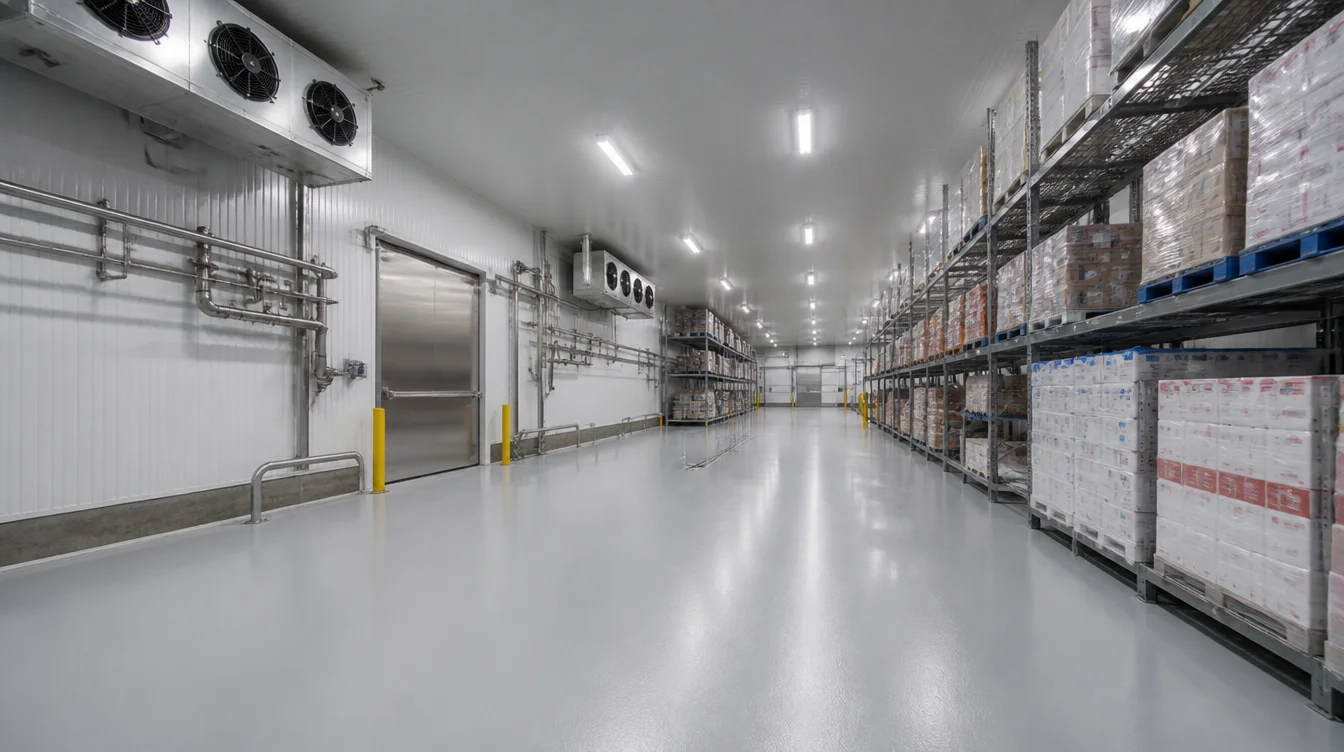
Commercial epoxy flooring for Nashville cold storage and food processing facilities has to handle a combination of stresses most other commercial spaces never face at once: constant temperature swings, sanitation-grade cleaning chemicals, and near-continuous moisture exposure. A standard warehouse epoxy system that performs well elsewhere often fails quickly in these environments, which is why cold storage and food processing floors get their own dedicated specification rather than a generic industrial coating.
Nashville's growing food and beverage distribution sector - supporting everything from regional grocery chains to restaurant supply operations - has made this a more common project than it once was. Facilities that started as ambient dry storage and later added refrigerated or frozen sections often discover that their original flooring wasn't specified for the new use, which is when a proper cold storage assessment becomes necessary rather than optional.
Why Cold Storage Floors Need a Different Epoxy Spec
Cold storage and food processing environments combine several demands that rarely appear together anywhere else:
- Repeated thermal cycling - floors move between ambient loading areas and sub-freezing storage constantly
- Frequent washdown cycles - sanitation protocols require regular cleaning with industrial-strength chemicals
- Standing moisture and condensation - temperature differentials create ongoing moisture exposure most warehouses don't see
- Strict sanitation compliance - food safety regulations require specific surface characteristics that general commercial epoxy doesn't guarantee
A coating built for one of these conditions but not the others tends to fail faster than expected. The right cold storage system is engineered to handle all four simultaneously, which is a meaningfully different specification than even a heavy-duty warehouse epoxy built for forklift traffic alone - durability against traffic is only one piece of what this type of floor needs to survive.
Forklift and pallet jack traffic still matters in these facilities too, often on top of everything else - cold storage warehouses move product constantly, and the flooring has to survive that wheel loading in addition to the thermal and sanitation demands unique to the environment. This is why cold storage specifications sometimes combine several performance requirements that would each be handled separately in a simpler facility, and why a one-size-fits-all industrial coating rarely holds up to the full combination of demands.
Thermal Shock Resistance Explained
Thermal shock resistance describes a coating's ability to withstand rapid, repeated temperature changes without cracking, delaminating, or losing adhesion to the slab underneath. A cold storage floor near a dock door might swing from a humid Nashville summer afternoon outside to sub-freezing temperatures inside within minutes, day after day. Standard epoxy resin, formulated for stable indoor temperatures, can become brittle and crack under this kind of repeated thermal stress.
NSF and Sanitation Compliance
Food processing facilities operate under strict sanitation standards, and the flooring plays a direct role in meeting them. NSF-compliant epoxy systems are formulated to resist the harsh cleaning chemicals used in daily washdown cycles, maintain a completely seamless surface with no cracks or joints where bacteria could establish, and hold up to the kind of aggressive, frequent cleaning that would degrade a standard commercial coating over time.
Cove base details - where the floor meets the wall - matter just as much as the floor itself in these environments. A properly installed integral cove base eliminates the 90-degree corner where standing water and contaminants would otherwise collect, curving the coating up the wall instead of leaving a hard seam at floor level.
Documentation matters for facilities operating under third-party food safety audits as well. Many food processing operations need to demonstrate their flooring meets specific sanitation standards as part of routine inspections, and working with a contractor who understands both the coating specification and the compliance paperwork saves time when audit season comes around, rather than scrambling to produce documentation after the fact.
Beyond the floor itself: Drains, trench systems, and floor-to-wall transitions all need to be compatible with the sanitation standards your facility operates under. These details are part of a proper cold storage flooring specification, not an afterthought handled separately.
Slip Resistance in Wet, Cold Environments
Condensation and frost are constants in cold storage, and a smooth, glossy floor becomes a serious slip hazard under those conditions. Slip-resistant additives - fine aggregate broadcast into the topcoat - create meaningful traction without compromising the seamless, easy-to-clean surface that sanitation compliance requires. This balance is more delicate than it sounds: too little texture and the floor stays slippery when wet or frosted; too much and the surface becomes difficult to sanitize thoroughly.
The right level of slip resistance also depends on where in the facility you're specifying it. A dry storage aisle with occasional moisture exposure needs less aggressive texture than a wash-down zone or a dock area where condensation forms constantly as product moves between temperature zones. A facility-wide walkthrough during the assessment phase identifies which areas need the most aggressive slip-resistant formulation and which can use a lighter touch, keeping cleaning labor manageable across the whole space rather than over-specifying texture everywhere.
Worker safety and liability are the practical drivers behind getting this right. A slip-and-fall incident in a cold storage facility isn't just a safety concern - it's a real operational and insurance cost that a properly specified floor helps prevent from the start, rather than addressing after an incident occurs.
| Requirement | Cold Storage Solution |
|---|---|
| Thermal cycling | Flexible resin system rated for repeated freeze-thaw stress |
| Sanitation compliance | NSF-compliant epoxy with integral cove base |
| Chemical resistance | Resin matched to specific washdown chemicals used |
| Slip resistance | Fine aggregate topcoat additive, balanced for cleanability |
These systems require more specialized formulation than a standard commercial or warehouse epoxy, which is why cold storage and food processing projects benefit from a contractor experienced with the specific combination of thermal, chemical, and sanitation requirements involved. A generic industrial coating specified without accounting for these factors is one of the most common reasons we get called in to repair or replace a cold storage floor within just a few years of its original installation.
See our commercial epoxy flooring Nashville page for the full range of systems we install, our urethane cement floor Nashville page for an alternative system well-suited to the heaviest thermal and chemical exposure, and our restaurant epoxy flooring Nashville page for related food-service specifications.
Many of the same phased-installation principles apply to other industrial settings - see our guide on manufacturing plant flooring for a related specification approach.